Strategies for Deploying AI in Food Manufacturing
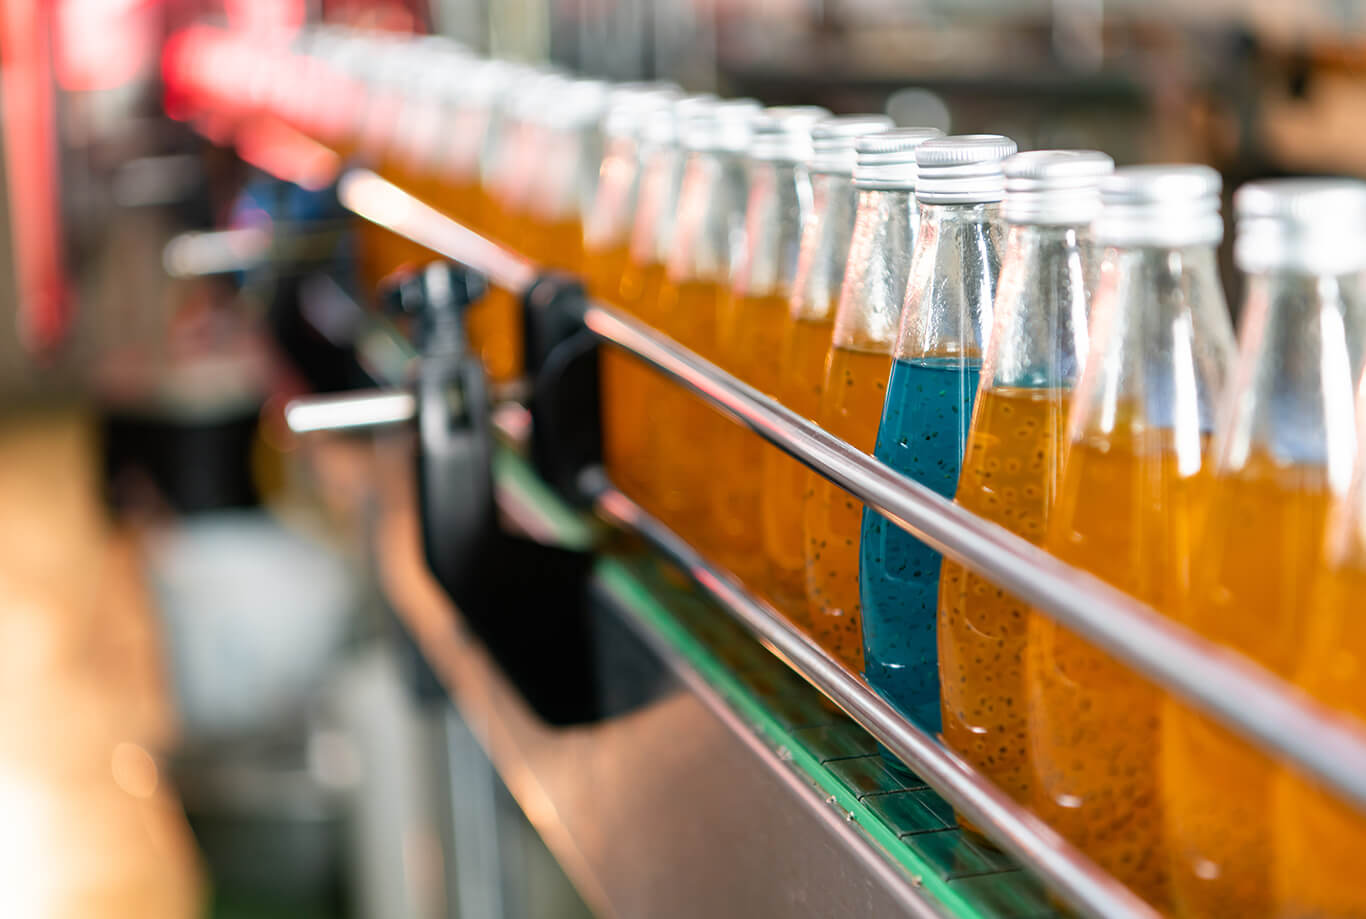
Food and beverage manufacturers generate more data than ever — from the line, the warehouse, and every store the product touches. AI in food manufacturing is what turns that data into decisions: faster problem detection, tighter compliance, and fewer surprises between the plant and the shelf. Used well, it doesn’t replace the people running your operation. It gives them a clearer picture, sooner, so they can act on it.
Why AI matters in food manufacturing
AI is exceptionally good at one thing: processing huge volumes of data fast. What it can’t do is problem-solve, innovate, or make the judgment calls your team makes every day. That’s exactly why the pairing works. When AI-driven data processing is combined with human decision-making, manufacturers see improved safety, streamlined operations, reduced manual labor, and more room for innovation.
The upside isn’t limited to the plant floor, either. Applied across the supply chain, AI-powered analytics can support revenue growth through more accurate demand forecasting, more relevant local assortments, personalized customer experiences, and sharper return on marketing and promotional spend. Organizations that use their data to move faster, reduce risk, and act with more confidence build an advantage that’s hard for competitors to close.
How is AI used in food and beverage manufacturing?
AI shows up across the manufacturing and field execution process in a few specific, high-value ways:
- Safety. AI-driven analysis of production and field data helps teams catch unsafe conditions earlier — before they become incidents, recalls, or compliance failures.
- Quality control. By analyzing data at scale, AI can pinpoint quality issues before they reach the consumer, protecting brand reputation and reducing costly rework.
- Compliance documentation. Manual food safety documentation is slow and error-prone. AI helps standardize and streamline how compliance conditions are recorded and tracked, saving time and reducing risk.
- Demand forecasting. Predictive analytics improve forecast accuracy, which means better assortments, less waste, and inventory that actually matches demand.
- Operational visibility. AI surfaces trends across the supply chain and manufacturing process that would otherwise stay buried in disconnected data sets — giving leaders the full picture instead of a partial one.
Getting started: how to implement AI in food manufacturing
Successful AI adoption doesn’t start with a full rollout — it starts with a plan.
- Set clear objectives first. Before implementing any AI or machine learning technology, enterprises need clarity on the specific business problem they’re solving. AI without a defined objective is just a science project.
- Start small. Begin with a controlled pilot — a single line, a single use case — where different approaches can be tested and measured before scaling.
- Train your team. AI is only as effective as the people using it. Give workers the training they need to work productively alongside new systems, so adoption sticks past the pilot phase.
Manufacturers that pair a sound AI strategy with real training see the payoff: fewer blind spots, better use of their people, and a stronger customer experience from plant to shelf.
See it in action
Ready to see how AI-powered data can work for your team? Read the white paper or request a demo to explore how FORM connects your field data, task management, and insights in one platform.
Frequently asked questions
What is AI used for in food manufacturing?
AI is used to analyze production and field data, improve safety and quality control, reduce manual work, and spot issues earlier — before they affect the consumer.
How does AI improve food safety and compliance?
It helps identify risks faster, document conditions more consistently, and support more reliable compliance tracking across locations.
What’s the difference between AI and automation in food manufacturing?
Automation handles repetitive, rules-based tasks. AI goes further — interpreting data, detecting patterns, and helping teams make better decisions.
Where does AI create the most value in food and beverage operations?
The biggest gains tend to show up in quality, compliance, operational visibility, labor efficiency, and faster response to emerging issues.
How can food manufacturers start using AI?
Start with a small, measurable use case, define the objective up front, and expand as you test results and train your team.
Does AI in food manufacturing apply to grocery retailers too?
Yes — many of the same principles apply downstream at the store level. In grocery, AI-powered insights help teams catch on-shelf availability issues, verify execution, and respond to problems faster, extending the same data-driven approach from the plant to the shelf.